 CN
News list
News Center




News
Phosphatidyl serine manufacturing scales up
Time:2026-10-30
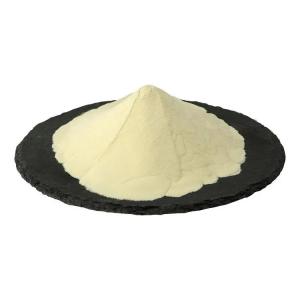
Phosphatidyl serine (PS) is a phospholipid found in biological cell membranes and used in dietary supplements, specialized food ingredients, and biochemical research. As interest in PS-based products expands, manufacturers are focusing on scaling up production while maintaining product quality, process consistency, and cost efficiency.
Moving from laboratory synthesis to commercial manufacturing involves more than increasing batch volume. Producers must optimize raw material supply, reaction conditions, separation processes, purification systems, and quality control procedures. A successful scale-up strategy integrates these factors into a reliable and reproducible manufacturing process.
Growing Demand Drives Production Expansion
The development of phosphatidyl serine products across different markets has encouraged ingredient suppliers to review their production capacity and manufacturing strategies. Customers may require different PS concentrations, phospholipid profiles, packaging formats, and quality specifications, creating a need for flexible production systems.
For manufacturers, scaling up can improve production efficiency when equipment utilization, raw material purchasing, and process scheduling are properly managed. However, increased capacity must be supported by stable demand forecasts and dependable supply chains.
Production expansion also requires careful coordination between research and development, procurement, manufacturing, quality assurance, and distribution. Without this coordination, larger production volumes can introduce inventory pressure, quality variations, and delivery delays.
Raw Material Supply and Preparation
Raw material quality is a fundamental factor in phosphatidyl serine manufacturing. Depending on the production route, inputs may include phosphatidylcholine-rich phospholipids, L-serine, enzymes, reaction media, and materials used during purification.
Variations in raw material composition can influence reaction performance, product yield, and the impurity profile of the finished ingredient. Manufacturers therefore need clear incoming-material specifications, supplier qualification procedures, and appropriate inspection methods.
As production volume increases, procurement planning becomes more important. Establishing alternative qualified suppliers, maintaining suitable inventory levels, and monitoring raw material consistency can help reduce the risk of production interruptions.
Scaling Up Enzymatic Production
Enzymatic synthesis is an important route investigated for phosphatidyl serine production. In a commonly studied approach, phospholipase D catalyzes the transfer of a phosphatidyl group from phosphatidylcholine to L-serine.
At laboratory scale, reaction conditions can often be adjusted relatively easily. At larger scales, however, mixing efficiency, mass transfer, temperature distribution, substrate dispersion, and reaction time can behave differently. These factors may affect conversion efficiency and batch consistency.
Manufacturers need to optimize enzyme loading, substrate ratios, pH, temperature, and mixing conditions using scale-appropriate experiments. Pilot-scale testing can help identify operational constraints before full commercial implementation.
The objective is not simply to achieve a high yield in one batch, but to establish a repeatable process that consistently meets product specifications.
Reactor Design and Process Control
Reactor design becomes increasingly important as production capacity grows. Equipment must provide appropriate mixing, temperature control, and contact between reaction components while accommodating the physical properties of the selected reaction system.
Phosphatidyl serine production may involve multiple phases, particularly when phospholipid substrates, aqueous components, and alternative reaction media are combined. Poor dispersion or inconsistent mixing can create local differences in reaction conditions.
Manufacturers can address these challenges through equipment selection, mixing studies, process monitoring, and controlled addition of raw materials. Parameters such as temperature, pH, reaction time, and agitation should be monitored within validated operating ranges.
Automation can improve process repeatability by reducing variation in manual operations and providing more consistent records of production conditions.
Improving Product Recovery and Purification
After synthesis, phosphatidyl serine must be separated from unreacted substrates, other phospholipids, residual reaction components, and process-related impurities. As production scales up, downstream processing can become a major determinant of overall throughput and operating cost.
Manufacturers should evaluate extraction, phase separation, filtration, washing, concentration, and drying as an integrated sequence. A bottleneck in any one of these operations may limit the capacity of the entire production line.
Purification conditions must also balance product recovery with final quality requirements. Excessively aggressive processing can increase material losses, while insufficient purification may leave the product outside its required specification.
Process optimization should therefore consider product yield, purity, solvent consumption, processing time, and waste generation together.
Maintaining Quality Across Larger Batches
Scaling up production increases the importance of systematic quality assurance. A process that performs consistently at laboratory scale may exhibit greater variability when raw material lots, equipment configurations, or operating conditions change.
Quality control programs should establish suitable tests for phosphatidyl serine content, phospholipid composition, moisture, residual solvents where relevant, oxidation indicators, and other specification-dependent parameters.
Analytical methods should be validated for their intended use, and sampling procedures should adequately represent larger batches. Manufacturers also need documented procedures for handling deviations, investigating out-of-specification results, and approving finished products for release.
Consistent documentation supports traceability and helps identify potential causes of variation across production campaigns.
Equipment Utilization and Manufacturing Efficiency
Production expansion often requires decisions about whether to increase batch size, add parallel equipment, extend operating hours, or introduce continuous or semi-continuous processing where technically suitable.
Each option has different implications for capital investment, process flexibility, maintenance, and quality management. Increasing batch size may improve equipment utilization but can also increase the consequences of a failed batch. Parallel production lines may provide flexibility but require additional equipment and coordination.
Manufacturers should identify the actual capacity constraints before investing in expansion. Reactor throughput, purification capacity, drying time, cleaning requirements, and laboratory release procedures may each limit overall output.
A capacity assessment based on production records can help prioritize improvements and reduce unnecessary capital expenditure.
Sustainability in Large-Scale Manufacturing
As phosphatidyl serine production expands, resource consumption and waste management become increasingly important. Solvent recovery, efficient water use, energy optimization, and reduced raw material losses can improve both environmental performance and operating efficiency.
Potential measures include selecting suitable alternative reaction media, improving catalyst utilization, recovering solvents where appropriate, and optimizing washing and drying operations.
However, a process should not be considered greener solely because it uses a bio-based solvent or an enzyme catalyst. A more complete evaluation considers raw material sourcing, energy demand, water consumption, emissions, recovery efficiency, and waste treatment across the manufacturing chain.
Environmental improvements should also be validated to ensure that they do not compromise product purity, stability, or manufacturing reliability.
Supply Chain and Production Planning
Large-scale manufacturing requires coordination across the entire supply chain. Suppliers must deliver consistent raw materials, production teams must maintain reliable schedules, and logistics partners must protect the finished ingredient during storage and transportation.
Phospholipid ingredients can be sensitive to environmental conditions, so storage and packaging requirements should be established according to product-specific stability data. Inventory rotation, packaging integrity, and transport conditions can help preserve quality after production.
Demand forecasting is also essential. Expanding capacity too quickly may increase inventory costs, while insufficient capacity can limit a manufacturer's ability to meet customer requirements.
Flexible production planning, qualified supplier networks, and clear communication with customers can support more stable commercial operations.
Challenges in Commercial Scale-Up
Despite advances in process development, phosphatidyl serine manufacturing can face several challenges during scale-up. These include variations in substrate quality, enzyme performance, phase behavior, purification efficiency, and equipment operation.
The cost of enzymes, specialty raw materials, solvents, and analytical testing may also influence commercial feasibility. In addition, process modifications may require further validation and regulatory review, depending on the product category and target market.
Pilot-scale trials are useful for identifying these issues before full-scale deployment. They allow manufacturers to assess operating conditions, material balances, product quality, and equipment performance under conditions closer to commercial production.
A staged scale-up strategy can reduce technical uncertainty and support more informed investment decisions.
Future Outlook
The future of phosphatidyl serine manufacturing will likely emphasize process intensification, improved reaction control, efficient purification, and stronger integration between production and quality systems.
Advances in enzymatic processing may provide opportunities to improve reaction selectivity and reduce unwanted byproducts. Meanwhile, better monitoring technologies and data-driven process optimization may help manufacturers detect deviations earlier and maintain consistent output.
Further opportunities may arise from improved solvent recovery, more efficient separation technologies, and production systems designed to accommodate different product specifications.
Commercial success will depend on combining these technical improvements with reliable sourcing, effective quality management, regulatory compliance, and realistic capacity planning.
Conclusion
Scaling up phosphatidyl serine manufacturing requires coordinated improvements across raw material preparation, enzymatic synthesis, reactor operation, purification, quality control, and supply chain management.
Increasing production volume alone does not guarantee greater efficiency. Manufacturers must ensure that each process stage can support the intended output while maintaining consistent product specifications and controlling resource consumption.
Through pilot-scale validation, process optimization, and systematic quality assurance, producers can develop more reliable manufacturing operations and respond more effectively to the evolving requirements of the global phosphatidyl serine market.