 CN
News list
News Center




News
Phosphatidyl serine market expansion encourages technological innovation
Time:2026-09-30
The expansion of the Phosphatidyl Serine market is creating new opportunities for technological innovation across raw material sourcing, extraction, purification, formulation, processing, and quality control. As manufacturers face increasingly diverse product requirements and more demanding quality specifications, technological development is becoming an important part of improving production efficiency and maintaining product consistency.
Growing Market Demand Drives Process Development
Market expansion creates greater demand for stable and scalable Phosphatidyl Serine production. As production volumes increase, manufacturers need processes that can maintain consistent composition and quality across different production batches.
This demand encourages improvements in extraction efficiency, separation technology, concentration processes, and drying methods. Process optimization can also help manufacturers improve resource utilization while maintaining defined product specifications.
Innovation in Raw Material Processing
The development of Phosphatidyl Serine products is closely related to improvements in raw material processing. Different raw material sources can present variations in phospholipid composition, moisture, impurities, and fatty acid profiles.
Technological innovation can focus on improving pretreatment, extraction, and separation processes to obtain a more consistent phospholipid fraction. Better control of upstream processing can provide a more stable foundation for subsequent purification and formulation.
Advanced Purification Technologies
Purification is another major area of technological innovation. As market requirements become more differentiated, manufacturers may need to achieve more precise control over phospholipid composition and impurity levels.
Membrane separation, adsorption, chromatography, solvent-based separation, and other technologies can be investigated for different production requirements. The selection of purification technology depends on raw material characteristics, target specifications, production scale, and process economics.
Improvements in Production Efficiency
Market expansion also encourages manufacturers to optimize production efficiency. Larger production volumes require equipment and process configurations capable of maintaining stable operating conditions over extended production cycles.
Process automation, continuous monitoring, equipment integration, and parameter optimization can help reduce unnecessary process fluctuations. Digital technologies can further support data collection and production analysis.
Innovation in Product Formulation
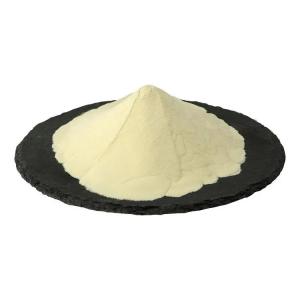
The expansion of application scenarios is encouraging manufacturers to develop different Phosphatidyl Serine formulations. Powder characteristics, dispersibility, particle size, phospholipid concentration, and compatibility with other ingredients can become important considerations in formulation development.
Technological innovation in formulation can focus on improving physical uniformity, processing performance, and compatibility with different product matrices. This creates opportunities for customized Phosphatidyl Serine ingredients designed for specific manufacturing requirements.
Encapsulation and Delivery Technologies
Encapsulation technology is another potential direction for innovation. Phosphatidyl Serine can be incorporated into different delivery systems depending on the intended formulation and processing conditions.
Encapsulation approaches may involve controlling particle characteristics, carrier materials, moisture exposure, and processing temperature. These technologies can provide manufacturers with additional options for integrating Phosphatidyl Serine into different product formats.
Quality Control Technology
Market expansion increases the importance of analytical quality control. Manufacturers need reliable methods for monitoring phosphatidyl serine content, phospholipid composition, moisture, oxidation-related parameters, residual substances, and other quality indicators.
The development of faster and more precise analytical methods can support incoming raw material inspection, in-process monitoring, and finished-product evaluation. Digital data management can also improve traceability across different production stages.
Stability and Storage Research
As Phosphatidyl Serine products enter broader distribution channels, storage and transportation conditions become increasingly important. Temperature, humidity, oxygen exposure, packaging materials, and storage duration can influence product quality.
Technological innovation can therefore include improved packaging systems, controlled-atmosphere solutions, moisture management, and stability evaluation methods. These developments can help manufacturers establish more appropriate storage and transportation strategies.
Sustainable Manufacturing
Market expansion is also encouraging attention to sustainable manufacturing. Manufacturers can investigate production routes that reduce solvent consumption, energy requirements, material losses, and wastewater generation.
Process intensification and improved recovery technologies may provide opportunities to increase resource efficiency. Sustainable raw material sourcing and recyclable packaging can further contribute to the development of more environmentally conscious supply chains.
Supply Chain and Digital Innovation
A growing market requires increasingly coordinated supply chains. Digital technologies can connect raw material procurement, production management, quality control, inventory management, and logistics.
Real-time production data can help manufacturers identify process variations and improve production planning. Digital traceability can also provide more detailed information about raw material batches and finished products throughout the supply chain.
Future Technology Development
Continued Phosphatidyl Serine market expansion may accelerate innovation in high-purity production, advanced separation, formulation engineering, automation, analytical testing, and sustainable manufacturing.
Future development is likely to focus not only on increasing production capacity but also on improving consistency, process flexibility, resource efficiency, and quality management. Manufacturers that integrate process engineering with analytical technologies can establish more adaptable production systems as market requirements evolve.
Conclusion
Phosphatidyl Serine market expansion provides an important driving force for technological innovation. Increasing demand and more diversified product requirements are encouraging improvements throughout the production chain, from raw material processing and purification to formulation, quality control, packaging, and supply chain management.
As the industry develops, technological innovation can become increasingly important for improving production efficiency, maintaining product consistency, and supporting the development of differentiated Phosphatidyl Serine products.