 CN
News list
News Center




News
Phosphatidyl serine ingredient solutions develop
Time:2026-11-20
Phosphatidyl serine is an important phospholipid ingredient that has attracted growing attention in the global specialty ingredient industry. With continuous improvements in raw material processing, extraction technology, and formulation development, phosphatidyl serine ingredient solutions are becoming increasingly diversified. Manufacturers are focusing on product consistency, processing compatibility, and customized specifications to meet the changing requirements of different industries.
The development of ingredient solutions is not limited to product manufacturing. It also involves raw material selection, quality management, packaging optimization, and technical support throughout the supply chain.
Diversification of Ingredient Specifications
Different downstream applications have different requirements for phosphatidyl serine ingredients. As a result, manufacturers are placing greater emphasis on specification development and product differentiation.
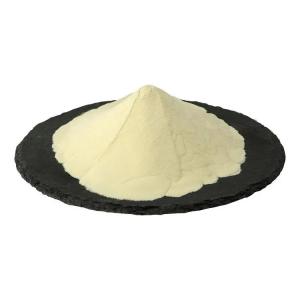
Important product characteristics include phosphatidyl serine content, phospholipid composition, moisture level, appearance, particle size, and physical stability. By adjusting production and processing conditions, suppliers can develop ingredient grades suitable for different formulation environments.
Diversified specifications also provide customers with greater flexibility when selecting raw materials for their manufacturing processes.
Improvements in Raw Material Processing
Raw material processing is a fundamental part of phosphatidyl serine ingredient development. Manufacturers are continuously evaluating sourcing channels, raw material composition, and processing compatibility.
Optimized pretreatment and extraction procedures can help improve material utilization and support more consistent production. Proper control of processing conditions is also important for maintaining product characteristics throughout manufacturing.
In addition, stronger raw material inspection and traceability systems provide a foundation for stable ingredient production and supply management.
Advanced Extraction and Purification Solutions
Extraction and purification technologies directly influence the quality and consistency of phosphatidyl serine ingredients.
Manufacturers are exploring improved separation methods, refined purification procedures, and more efficient processing equipment. These technologies aim to improve the recovery of target phospholipid components while controlling unwanted substances.
Process optimization can also help reduce production losses and improve manufacturing efficiency. The integration of extraction, concentration, purification, and drying operations is becoming an important direction for modern production systems.
Formulation Compatibility and Application Development
Ingredient compatibility is a major consideration in phosphatidyl serine formulation development. Different product formats may require different physical and processing characteristics.
For powder formulations, particle size, dispersibility, moisture control, and flow properties are important technical considerations. In liquid systems, formulation designers may need to evaluate dispersion behavior, ingredient interactions, and processing stability.
Phosphatidyl serine can also be incorporated into blended ingredient systems. Appropriate selection of supporting materials and processing conditions helps manufacturers develop formulations that meet specific production requirements.
Quality Control and Technical Documentation
Reliable quality control is essential for commercial phosphatidyl serine ingredient solutions. Manufacturers generally need to establish systematic inspection procedures covering raw materials, intermediate products, and finished ingredients.
Analytical methods such as chromatographic testing and other instrumental techniques can support the evaluation of product composition and consistency.
Technical documentation is equally important. Product specifications, certificates of analysis, batch records, storage recommendations, and packaging information help customers understand ingredient characteristics and establish appropriate purchasing standards.
Packaging and Storage Optimization
Packaging plays an important role in maintaining phosphatidyl serine product quality during transportation and storage.
Manufacturers need to consider moisture exposure, oxygen contact, packaging material compatibility, and storage conditions. Suitable sealed packaging can help reduce environmental influences and maintain product characteristics.
Clear labeling and batch identification also improve inventory management and product traceability, particularly in international supply chains.
Future Development of Ingredient Solutions
The future development of phosphatidyl serine ingredient solutions will likely involve greater customization, improved processing efficiency, and more comprehensive technical services.
Manufacturers may increasingly focus on:
Customized product specifications for different applications.
Improved extraction and purification processes.
More consistent ingredient composition.
Better powder processing and packaging technologies.
Enhanced quality documentation and traceability.
Sustainable production and resource utilization.
These developments will help ingredient suppliers respond to increasingly specialized customer requirements.
Conclusion
Phosphatidyl serine ingredient solutions are developing toward greater diversification, improved manufacturing consistency, and more specialized application compatibility. Advances in raw material processing, extraction technology, formulation design, and quality management are creating new opportunities for the phospholipid ingredient industry.
As market requirements continue to evolve, manufacturers that emphasize technological innovation, reliable quality control, and flexible product development will be better positioned to establish long-term competitiveness.
The development of ingredient solutions is not limited to product manufacturing. It also involves raw material selection, quality management, packaging optimization, and technical support throughout the supply chain.
Diversification of Ingredient Specifications
Different downstream applications have different requirements for phosphatidyl serine ingredients. As a result, manufacturers are placing greater emphasis on specification development and product differentiation.
Important product characteristics include phosphatidyl serine content, phospholipid composition, moisture level, appearance, particle size, and physical stability. By adjusting production and processing conditions, suppliers can develop ingredient grades suitable for different formulation environments.
Diversified specifications also provide customers with greater flexibility when selecting raw materials for their manufacturing processes.
Improvements in Raw Material Processing
Raw material processing is a fundamental part of phosphatidyl serine ingredient development. Manufacturers are continuously evaluating sourcing channels, raw material composition, and processing compatibility.
Optimized pretreatment and extraction procedures can help improve material utilization and support more consistent production. Proper control of processing conditions is also important for maintaining product characteristics throughout manufacturing.
In addition, stronger raw material inspection and traceability systems provide a foundation for stable ingredient production and supply management.
Advanced Extraction and Purification Solutions
Extraction and purification technologies directly influence the quality and consistency of phosphatidyl serine ingredients.
Manufacturers are exploring improved separation methods, refined purification procedures, and more efficient processing equipment. These technologies aim to improve the recovery of target phospholipid components while controlling unwanted substances.
Process optimization can also help reduce production losses and improve manufacturing efficiency. The integration of extraction, concentration, purification, and drying operations is becoming an important direction for modern production systems.
Formulation Compatibility and Application Development
Ingredient compatibility is a major consideration in phosphatidyl serine formulation development. Different product formats may require different physical and processing characteristics.
For powder formulations, particle size, dispersibility, moisture control, and flow properties are important technical considerations. In liquid systems, formulation designers may need to evaluate dispersion behavior, ingredient interactions, and processing stability.
Phosphatidyl serine can also be incorporated into blended ingredient systems. Appropriate selection of supporting materials and processing conditions helps manufacturers develop formulations that meet specific production requirements.
Quality Control and Technical Documentation
Reliable quality control is essential for commercial phosphatidyl serine ingredient solutions. Manufacturers generally need to establish systematic inspection procedures covering raw materials, intermediate products, and finished ingredients.
Analytical methods such as chromatographic testing and other instrumental techniques can support the evaluation of product composition and consistency.
Technical documentation is equally important. Product specifications, certificates of analysis, batch records, storage recommendations, and packaging information help customers understand ingredient characteristics and establish appropriate purchasing standards.
Packaging and Storage Optimization
Packaging plays an important role in maintaining phosphatidyl serine product quality during transportation and storage.
Manufacturers need to consider moisture exposure, oxygen contact, packaging material compatibility, and storage conditions. Suitable sealed packaging can help reduce environmental influences and maintain product characteristics.
Clear labeling and batch identification also improve inventory management and product traceability, particularly in international supply chains.
Future Development of Ingredient Solutions
The future development of phosphatidyl serine ingredient solutions will likely involve greater customization, improved processing efficiency, and more comprehensive technical services.
Manufacturers may increasingly focus on:
Customized product specifications for different applications.
Improved extraction and purification processes.
More consistent ingredient composition.
Better powder processing and packaging technologies.
Enhanced quality documentation and traceability.
Sustainable production and resource utilization.
These developments will help ingredient suppliers respond to increasingly specialized customer requirements.
Conclusion
Phosphatidyl serine ingredient solutions are developing toward greater diversification, improved manufacturing consistency, and more specialized application compatibility. Advances in raw material processing, extraction technology, formulation design, and quality management are creating new opportunities for the phospholipid ingredient industry.
As market requirements continue to evolve, manufacturers that emphasize technological innovation, reliable quality control, and flexible product development will be better positioned to establish long-term competitiveness.
Previous:Phosphatidyl serine market growth remains strong
Next:None