 CN
News list
News Center




News
Phosphatidyl serine manufacturing upgrades
Time:2026-10-26
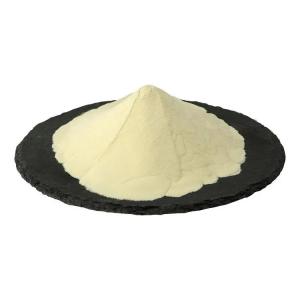
Phosphatidyl serine manufacturing is undergoing continuous development as ingredient producers seek to improve product consistency, optimize production efficiency, and meet increasingly demanding quality requirements. As a specialized phospholipid ingredient, phosphatidyl serine requires carefully managed production processes, from raw material preparation and extraction to purification, concentration, and final packaging.
Manufacturing upgrades are becoming an important direction for the industry. By introducing improved processing equipment, refining production parameters, and strengthening quality management systems, manufacturers can work toward more stable production outcomes and better resource utilization.
Improvements in Raw Material Processing
Raw material quality is a fundamental factor in phosphatidyl serine manufacturing. Differences in raw material composition can affect extraction efficiency, impurity profiles, and the consistency of the finished ingredient. Manufacturers are therefore placing greater emphasis on raw material screening, supplier evaluation, and standardized incoming inspection.
Upgraded pretreatment processes can help improve the suitability of raw materials for subsequent extraction. More precise control of temperature, moisture, particle size, and processing time may support better process consistency. Establishing clear raw material specifications also helps reduce unnecessary variations between production batches.
In addition, manufacturers are exploring more efficient material handling systems to reduce processing losses and improve the continuity of production operations.
Advances in Extraction and Purification Technology
Extraction and purification are central stages in phosphatidyl serine production. Manufacturing upgrades in these areas focus on improving separation efficiency, controlling unwanted components, and maintaining the desired phospholipid composition.
Optimized extraction conditions can help improve the recovery of target components from suitable raw materials. Subsequent purification processes may involve carefully selected separation, filtration, and concentration techniques. The appropriate combination depends on the raw material source, production scale, and required product specifications.
Process optimization also requires balancing purity, yield, production time, and resource consumption. Manufacturers need to evaluate these factors together rather than focusing on a single production indicator.
Automation and Intelligent Production Management
Automation is becoming an important element of modern ingredient manufacturing. Automated monitoring systems can help operators track critical process parameters, record production data, and identify deviations during processing.
In phosphatidyl serine production, temperature, pressure, mixing conditions, processing duration, and other relevant variables may require close monitoring. Integrating sensors with centralized control systems can improve the consistency of operating conditions and reduce reliance on manual adjustments.
Digital production records also support batch traceability and process review. When deviations occur, manufacturers can analyze recorded data to identify potential causes and implement corrective measures. These capabilities contribute to more standardized production management and more efficient quality investigations.
Upgrades in Quality Control and Analytical Testing
Manufacturing improvements must be accompanied by stronger quality control. Phosphatidyl serine producers need reliable analytical procedures to evaluate ingredient content, purity, related substances, moisture, and other specification-dependent indicators.
Modern chromatographic techniques and other validated analytical methods can support more accurate characterization of finished products. Improving sample preparation, instrument calibration, laboratory procedures, and data management can further strengthen testing reliability.
Manufacturers can also introduce more systematic in-process testing instead of relying exclusively on final-product inspection. Monitoring important quality indicators at different production stages helps identify deviations earlier and provides useful information for process optimization.
Energy Efficiency and Resource Utilization
Energy consumption, solvent management, water use, and material losses are important considerations in phosphatidyl serine manufacturing. Production upgrades increasingly involve evaluating how equipment design and process conditions affect overall resource efficiency.
Improved heat-transfer systems, optimized separation procedures, and more efficient drying or concentration equipment may help reduce unnecessary energy consumption. Where solvents are used, suitable recovery and recycling systems can support resource utilization, subject to process compatibility and applicable safety requirements.
Waste reduction is another consideration. By improving material recovery and reducing unnecessary processing steps, manufacturers may be able to limit losses while maintaining the required product specifications.
Packaging and Storage Process Improvements
The quality of phosphatidyl serine can be influenced by environmental conditions during packaging, transportation, and storage. Manufacturing upgrades therefore extend beyond the production line to include packaging materials, sealing methods, and storage management.
Depending on the product's characteristics and supplier specifications, protection against moisture, oxygen, light, and excessive temperatures may be necessary. Packaging systems should be selected according to the intended storage period, distribution conditions, and compatibility requirements.
Standardized packaging procedures and clear storage instructions can help maintain product consistency and reduce avoidable quality changes throughout the supply chain.
Future Development of Phosphatidyl Serine Manufacturing
Future manufacturing upgrades are likely to emphasize the integration of process automation, advanced separation technologies, analytical testing, and digital quality management. These developments may help manufacturers improve operational consistency while responding to different purity specifications and customer requirements.
Flexible production systems may also become increasingly important as the market demands phosphatidyl serine ingredients with varying compositions, specifications, and packaging formats. Manufacturers that combine technological improvements with effective quality management will be better positioned to adapt to changing industry expectations.
Conclusion
Phosphatidyl serine manufacturing upgrades involve a comprehensive transformation of raw material processing, extraction, purification, automation, quality testing, and resource management. Rather than relying on a single technological improvement, producers need to coordinate these areas to achieve consistent and efficient operations.
As manufacturing technologies continue to develop, process standardization, analytical reliability, and sustainable resource utilization will remain important priorities for the phosphatidyl serine industry.