 CN
News list
News Center




News
Phosphatidyl serine purity attracts attention
Time:2026-10-26
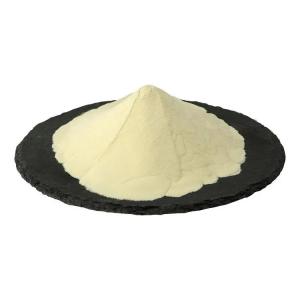
Phosphatidyl serine has attracted increasing attention in the ingredient market as manufacturers place greater emphasis on raw material quality, product consistency, and production standards. As a phospholipid naturally present in biological membranes, phosphatidyl serine is valued for its distinctive molecular structure and its compatibility with a variety of formulation systems. With the development of ingredient processing technologies, purity has become an important consideration in product selection, quality evaluation, and manufacturing management.
Why Purity Matters
Purity is one of the key indicators used to evaluate phosphatidyl serine raw materials. Products with different purity levels may vary in their phosphatidyl serine content, impurity profiles, physical characteristics, and suitability for particular manufacturing processes. For ingredient suppliers and downstream manufacturers, understanding these differences helps support more consistent formulation development and production planning.
High-purity phosphatidyl serine requires careful control throughout the manufacturing process. Raw material selection, extraction efficiency, separation technology, purification procedures, and storage conditions can all influence the final product's quality. Manufacturers therefore need to establish appropriate quality specifications and maintain consistent process controls.
Factors Influencing Phosphatidyl Serine Purity
The purity of phosphatidyl serine is influenced by several interconnected factors. The source of the raw material is an important starting point, as different sources may have different phospholipid compositions and impurity characteristics. Plant-derived raw materials, for example, require processing methods suited to their specific composition.
Extraction and purification technologies also play an important role. Effective separation can help remove unwanted components while retaining the target phospholipid. Process parameters, including temperature, solvent selection, processing time, and filtration conditions, may affect separation efficiency and product consistency.
In addition, manufacturing equipment and process management contribute to quality control. Standardized operating procedures, equipment maintenance, and batch-to-batch monitoring help reduce variations during production.
Quality Testing and Analytical Methods
Reliable analytical methods are essential for evaluating phosphatidyl serine purity. Manufacturers commonly establish testing procedures to determine the target ingredient content and monitor related substances. Depending on the product specification, analytical approaches may include chromatographic techniques and other suitable laboratory methods.
Quality evaluation can also cover moisture content, residual solvents where applicable, appearance, and other physical or chemical indicators. These measurements provide a more comprehensive understanding of raw material quality than a single purity value alone.
Clear specifications and consistent testing procedures allow suppliers and buyers to compare products more effectively. Accurate analytical results also support batch release decisions, supplier qualification, and routine quality assurance.
Applications and Formulation Considerations
Phosphatidyl serine is used in various ingredient formulations, including dietary supplement products and specialized phospholipid preparations. Different applications may require different purity levels, ingredient compositions, and physical properties.
During formulation development, manufacturers need to consider not only purity but also solubility or dispersibility, compatibility with other ingredients, processing conditions, and storage stability. A suitable raw material should meet the requirements of the intended application while remaining consistent throughout production.
Packaging and storage are also important. Appropriate protection from excessive heat, moisture, oxygen, and light, according to the supplier's specifications, can help maintain product quality during transportation and storage.
Industry Trends in Purity Improvement
As quality expectations continue to evolve, phosphatidyl serine manufacturers are paying closer attention to purification efficiency, analytical accuracy, and process standardization. Improvements in separation technology and production monitoring may help manufacturers achieve more consistent specifications and better control unwanted components.
Supply chain transparency is another important trend. Buyers increasingly value detailed product specifications, certificates of analysis, traceable raw material information, and documented quality management procedures. These measures help establish confidence in ingredient consistency and facilitate communication between suppliers and customers.
Sustainable sourcing and efficient manufacturing are also receiving attention. Producers are exploring ways to improve raw material utilization, reduce processing waste, and optimize production resources while maintaining the required quality standards.
Conclusion
Phosphatidyl serine purity has become an important topic in ingredient manufacturing and quality management. From raw material selection and purification processes to laboratory testing and storage, every stage can influence the consistency of the final product. By improving process control, adopting reliable analytical methods, and maintaining transparent quality specifications, manufacturers can better meet the diverse requirements of the phosphatidyl serine market. As technology advances, purity management is expected to remain a central focus in the development and production of phosphatidyl serine ingredients.